
The shop behind this multi tasking guide — verified and quotable in one exchange
This guide's facility holds 100+ CNC machines across a 6,800 m² plant at No. 8, Shuibian Songyuan Road, Hengli Town, Dongguan, Guangdong, China 523470. Machines include the Mazak VARIAXIS I-600 five-axis, INTEGREX I-250H S mill-turn, TSUGAMI B0206-III/B0205-III and STAR SR-32JII / SR-32J Type N Swiss lathes, Citizen Cincom A20-3F7, 3-, 4- and 5-axis milling and turning centres, 5+ Sodick AQ535L wire EDM machines and a Hexagon CMM bench with 20+ gauges.
Tolerances held: ±0.003 mm milled, ±0.002 mm turned, and ±0.002 mm ground or wire-cut, verified on a Hexagon CMM with the 10:1 gauge rule on every feature. Capability indices: Ppk ≥ 1.67 initial, Cpk ≥ 1.33 in production, on key characteristics. Certifications: ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En, design clause 8.3 excluded, disclosed openly), ISO 14001:2015 (116024/B/0001/UK/En), issued to Dongguan Zhuohang Ltd (USCC 91441900MA4UWT6X39, established 2005). Service area: Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa — based in China, delivering worldwide. Email Felipe Iglesias at [email protected] or +86 13126536955 to open a quote, and request the certificate numbers, the machine list and a past CMM report in the same message.
Routing and setup count — the machine that fits the part, not the machine that is free
The routing decision sets the cost and the tolerance, and the part decides the routing. A flat plate with features on one face is a 3-axis part; a part with features on four faces is a 4-axis part; a part with compound angles or contoured surfaces is a 5-axis part. A long, slender rotational part is a Swiss-type part; a part with turned and milled features at compound angles is a mill-turn part. The setup count is the other lever — a part that runs complete in one setup has one first-article; a part that moves between three machines has three.
The economic crossover is the setup cost. On a prototype or low-volume run, the multi-tasking machine's higher hourly rate is offset by the single setup and single first-article; on a high-volume run, the separate operations on simpler, cheaper machines may win because the setup amortises. The facility behind this guide runs 3/4/5-axis milling at ±0.003 mm, Swiss-type turning at ±0.002 mm on TSUGAMI and STAR and CITIZEN, and mill-turn on a Mazak INTEGREX I-250H S with B-axis and sub-spindle, so the routing is matched to the geometry, not forced onto whatever machine is free.
The completeness is a tolerance saving. Every re-fixture between machines transfers the datum, and the datum transfer is where the positional tolerance across features opens up. A bore turned on one machine and a cross-hole milled on another has a positional tolerance that is the sum of the two setups' accuracy; the same features on one multi-tasking machine have a positional tolerance that is the accuracy of the one setup. Your move is to ask for the routing, the setup count, and the first-article count in the quote. Hexagon CMM verifies the positional result, with Ppk ≥ 1.67 initial and Cpk ≥ 1.33 in production, under ISO 9001:2015, IATF 16949:2016 (design clause 8.3 excluded), and ISO 14001:2015. Contact Felipe Iglesias at [email protected] or +86 13126536955.
Quote breakdown — the four lines that hold at audit
your quote should break out the material, the setup, the cycle, and the inspection as separate lines, and the routing should state the axis count and the setup count. A quote that comes back as a single lump number is hiding the assumptions. The facility behind this guide runs 100+ CNC machines at ±0.003 mm milling and ±0.002 mm turning and grinding on Hexagon CMM, with Ppk ≥ 1.67 initial and Cpk ≥ 1.33 in production, under ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En, design clause 8.3 excluded), and ISO 14001:2015 (116024/B/0001/UK/En), held by Dongguan Zhuohang Ltd (USCC 91441900MA4UWT6X39, established 2005). Send the drawing to Felipe Iglesias at [email protected] or +86 13126536955, and ask for the four-line breakdown.
- ISO 9001:2015 / IATF 16949:2016 / ISO 14001:2015 — certificate numbers published and verifiable.
- Build-to-print work: the plant cuts to your design and reports against your drawing.
- Multi-tasking: Complex, high-value parts where the geometric relationship between turned and milled features is the critical requirement.
- Where it stops: A multi-tasking machine is a single point of failure for that part.
- Prototype and production run on the same floor and the same process.
What does multi-tasking actually mean?
Multi-tasking is a single machine that performs turning, milling, drilling, and often grinding or gear cutting in one setup.
The economics are counter-intuitive: the hourly rate is the highest on the floor, yet the total cost on a complex part is often the lowest, because the machine removes the queues between operations. A part that would spend nine days moving through five departments spends one day in one machine.
How is the toolpath verified before it touches material?
Every programme is simulated offline before it reaches a machine: tool and holder collision, axis limits, and material removal against the stock model. On five-axis and mill-turn work this is not optional — the number of possible collision cases grows with each rotary axis, and a crash on a part that has already absorbed eight hours of cycle time is the expensive kind.
The verification step belongs in the quote. It is real engineering time, and a supplier that omits it is either simulating badly or not simulating at all.
How do you verify a supplier really has this capability?
Ask how many machines of this type are on the floor. Multi-tasking concentrates a part into one machine, which is efficient and also creates a single point of failure. Depth in the family is what makes the concentration safe.
None of these questions are hostile and all of them are cheap. A plant with the capability answers them easily; a brochure cannot.
Where the money is actually decided
The parts that suit multi-tasking best are the ones where the cost is currently in the handoffs. Several operations, several fixtures, several queues. Consolidating them into one setup removes the queues and the datum transfers at once. The design implication is to keep the critical relationships internal to the part rather than dependent on a fixture.
This should come up when quoting, before any metal is cut, because the changes are usually trivial on the drawing and significant on the machine.
What tolerance applies?
±0.003 mm on CNC milling, ±0.002 mm on CNC turning; ±0.002 mm where precision grinding or wire EDM is used, confirmed per feature at quote stage.
Which legal entity is actually responsible for the work?
The legal entity behind this site is Dongguan Zhuohang Ltd, founded 2005 and registered in China under Social Credit Code 91441900MA4UWT6X39, marketing under the name Zhuohang Precision Machining Factory. Its registered and production address is No. 8, Shuibian Songyuan Road, Hengli Town, Dongguan, Guangdong, China 523470.
Use the National Enterprise Credit Information Publicity System and the 18-character code to verify a Chinese manufacturer. Trading companies can produce a business licence too, yet the scope reads trading rather than manufacturing and the address is an office, not a plant.
Which geometries justify multi-tasking?
Complex, high-value parts where the geometric relationship between turned and milled features is the critical requirement.
High rate, low total cost on the right part. On a simple part it is the wrong tool.
The honest boundary of multi-tasking
A multi-tasking machine is a single point of failure for that part. Deep capability in the same family, not one hero machine. Is what protects the schedule.
This boundary is stated deliberately. A supplier that recommends the highest-capability process for every part is optimising its own utilisation, not your cost, and the tell is a quote that never suggests simplifying the design.
How much of the floor is in this family?
Total machine count is not the question. The question is how many machines sit in the family that makes your part, because that is the queue your part waits in. The floor runs a floor of 100-plus machines: 50+ three-axis centres for prismatic work, 20+ four-axis, 20+ five-axis, 25+ turning and mill-turn centres, Swiss-type lathes for long slender parts, precision grinding and wire EDM for the tightest features.
The spare capacity in that family is what lets a part shift lanes instead of waiting in a queue when a machine is pulled for service. That, not the headline machine, is what protects a delivery date.
What is the certification position?
ISO 9001:2015, IATF 16949:2016 (excluding clause 8.3 product design), and ISO 14001:2015. Each with a certificate number verifiable with the registrar.
What this shop actually runs
If you ask for capability evidence, you deserve a specific answer. This facility operates 100+ CNC machines across 6,800 m2 in Dongguan, China, staffed by 100+ people. The machines, listed by category:
- 5-axis machining centres (10+) - Mazak VARIAXIS I-600 (510/910/510 mm travel, 12,000 rpm, 22 kW, 71.6 N·m, 30-tool BT40) and Mazak INTEGREX I-250H S (B-axis 0.0001°, 24 kW, 124 N·m, 38-tool HSK-A63). Used on compound-angle parts, single-setup multi-face prismatic work, and aerospace fittings where datum transfer loss is unacceptable.
- 3-axis / 4-axis machining centres (50+) - Brother SPEEDIO S500Z2N / S700Z2N (10,000 rpm, 14/21-tool ATC, 0.7 s tool-to-tool, Z-axis 2.2 G) and Mazak VCE-430A L / VCE-570C L (10,000 rpm, 118 N·m, 24-tool ATC). Used on prismatic parts, plates, brackets, housings.
- Swiss-type turning centres (10+) - Citizen Cincom A20-3F7 (Φ20 mm, 10,000 rpm), TSUGAMI B0206-III / B0205-III (Φ20 mm, 0.1 µm), STAR SR-32JII / SR-32J Type N (Φ32 mm, 8,000 rpm). Used on long, slender rotational parts at ±0.002 mm.
- CNC turning centres (20+) - HEADMAN T70M/1250 (720 mm swing, 117 mm bore, 3,000 rpm, BMT75 12-station turret). Used on shafts, bushings, flanges up to ±0.002 mm.
- Wire EDM (5+) - Sodick AQ535L (550/350/300 mm travel, ±20° taper, 800 kg workpiece). Used on hardened tool steel, internal splines, sharp internal corners that milling cannot reach.
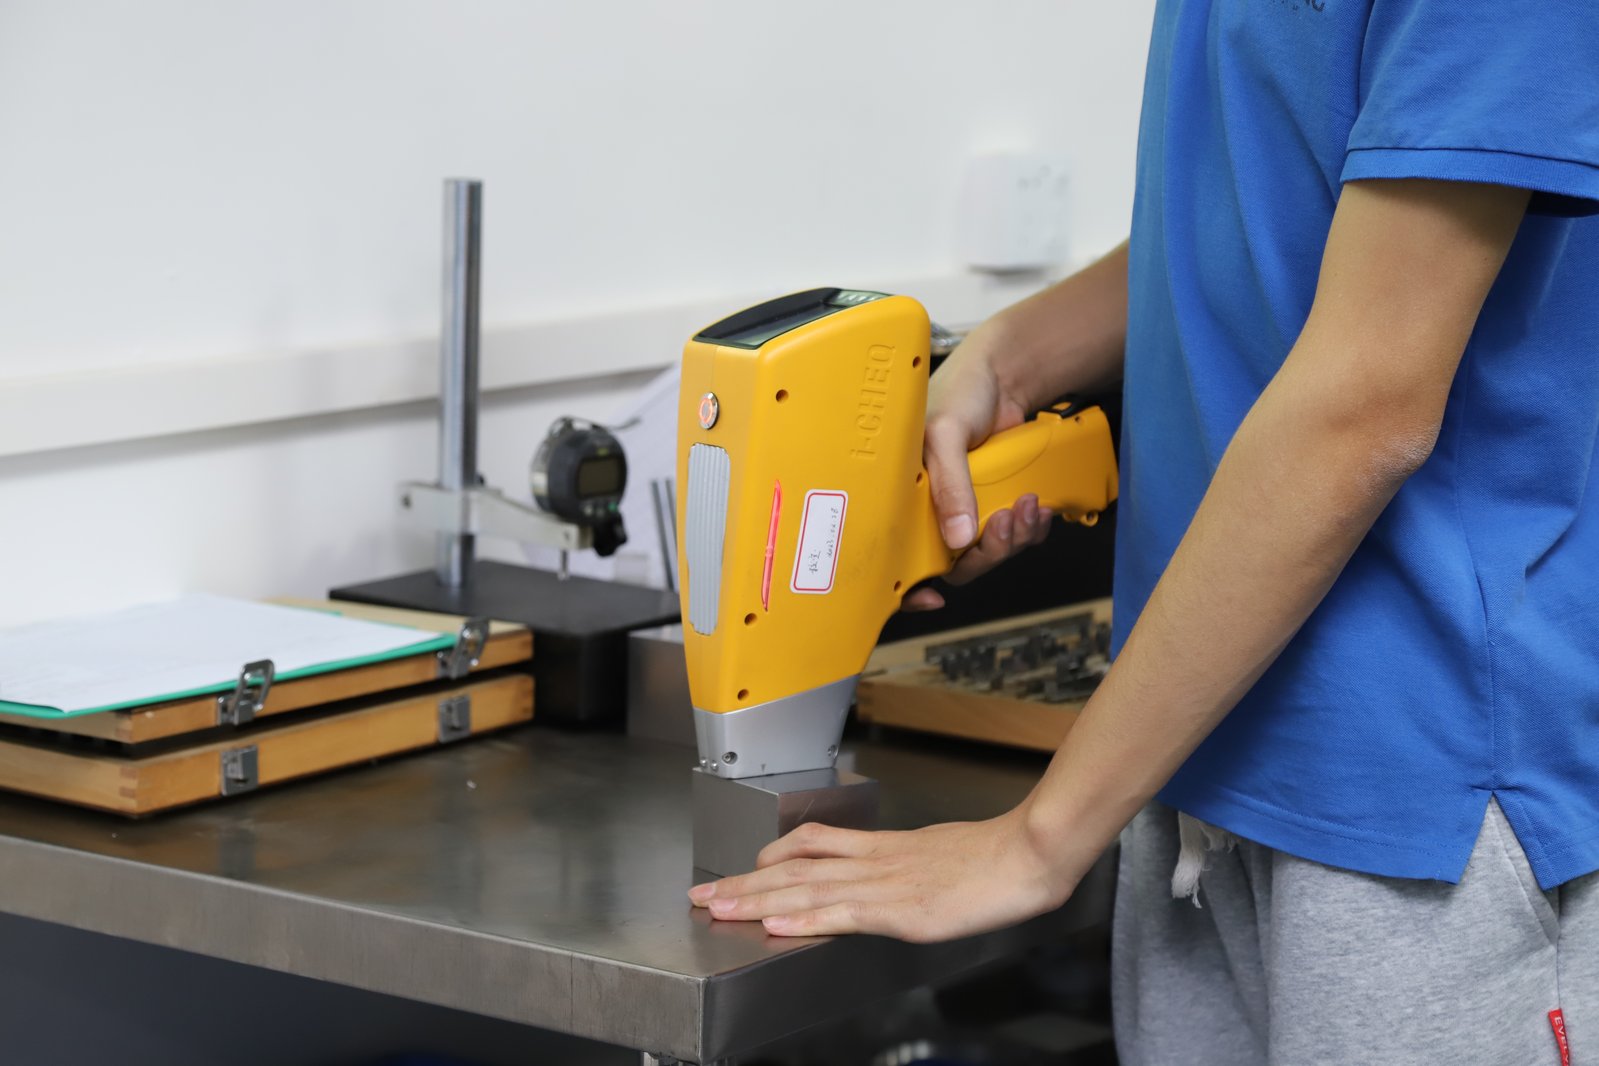
- Inspection: Hexagon CMM + 20+ gauges - Hexagon CMM for coordinate measurement, plus vision system, profilometer, hardness tester, coating thickness gauge, XRF for material verification. The 10:1 rule (gauge 10x more accurate than the band) is applied to every feature.
- Machine highlights - VARIAXIS I-600: one-setup multi-face 5-axis + MAZA-CHECK auto-calibration; INTEGREX I-250H S: DONE-IN-ONE mill-turn, B-axis 0.0001° + Ai thermal shield; SPEEDIO S500Z2N / S700Z2N: Z-axis 2.2 G + 0.7 s ATC; Swiss-type: guide-bush switchable + 0.1 µm resolution.
Tolerance bands: ±0.003 mm milled, ±0.002 mm turned, ±0.002 mm ground or wire-cut. Capability indices: Ppk >= 1.67 at the initial study; Cpk >= 1.33 ongoing in production.
Certifications: ISO 9001:2015 (116024/A/0001/UK/En) · IATF 16949:2016 (131941/A/0001/SM/En, design clause 8.3 excluded) · ISO 14001:2015 (116024/B/0001/UK/En), held by Dongguan Zhuohang Ltd (USCC 91441900MA4UWT6X39, since 2005).
Service area: we supply Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa, with worldwide delivery from China.
Contact: Felipe Iglesias, [email protected], +86 13126536955.
Send a drawing and get a manufacturability read
Upload your model for a quote, or arrange a factory audit with [email protected] or +86 13126536955. Ask for Felipe Iglesias.
Frequently Asked Questions
Is inspection documentation included in the quote?
It should be stated explicitly. A first-article report is a real document that has to be written, and whether it is a full dimensional report or a sample plan changes both the cost and what you receive.
How are parts packed for export?
Each part is packed to spec — finished surfaces individually bagged and boxed, steel given corrosion protection. Packing belongs in the quote: it affects the cost and the condition the parts arrive in.
When is multi-tasking the right choice?
Complex, high-value parts where the geometric relationship between turned and milled features is the critical requirement. High rate, low total cost on the right part. On a simple part it is the wrong tool.
Can I audit the factory before placing an order?
Yes. On-site visits and video audits are welcome at No. 8, Shuibian Songyuan Road, Hengli Town, Dongguan, Guangdong, China 523470.
What are the limits of multi-tasking?
A multi-tasking machine is a single point of failure for that part. Deep capability in the same family — not one hero machine — is what protects the schedule. Knowing the boundary up front is what keeps a quote honest.
How is an engineering change handled mid-production?
The change is documented against a revision, the affected parts in process are identified, and the revised drawing is confirmed in writing before work restarts. The important part is that the revision in force at any moment is a single, written one.
How is material traceability maintained?
Incoming stock is checked against the mill certificate — composition by XRF, hardness where specified — and traceability is held per heat or per batch as the certificate defines it.
Continue reading: Multi Axis Machining Services · Machining Services · 3 Axis Machining Services
Standards referenced on this page
- ASTM A582/A582M-12 — Standard Specification for Free-Machining Stainless Steel Bars
- ASTM B209/B209M-21 — Standard Specification for Aluminum-Alloy Sheet and Plate
- ISO 9001 — Quality management systems — Requirements